What are Thermoplastic Elastomers
TPEs combine the flexibility and elasticity of rubber with the processability of thermoplastics. Unlike traditional rubber, which requires vulcanization, TPEs can be melted and reformed multiple times without losing their properties, making them ideal for injection molding.

Key properties include:
- Excellent flexibility and elasticity: TPEs can stretch and return to their original shape, similar to rubber.
- Tensile strength: TPEs can withstand pulling forces without breaking, helping molded parts maintain their structural integrity during use.
- Resistance to heat, oils, and chemicals: They maintain performance in harsh environments.
- UV resistance: UV-resistant TPE grades can withstand prolonged sunlight exposure with reduced degradation, making them suitable for outdoor applications.
- Good colorability and transparency options: Allow for aesthetic customization.
- Recyclability: TPE production does not release harmful substances like dioxins and can be reprocessed, reducing waste.
- Cost-effectiveness: Compared to traditional rubbers, TPEs offer economic benefits in large-scale production.
- Design flexibility: TPEs can be molded into complex shapes, offering a range of hardness levels to meet diverse needs.
Disadvantages of TPEs include:
- Limited load-bearing capacity: TPEs are generally softer and less rigid than structural plastics, making them less suitable for applications requiring high stiffness.
- Compression set: Some TPE grades may not fully recover their original shape after prolonged compression, affecting long-term sealing performance.
- Material compatibility limitations: TPEs do not bond equally well to all rigid plastics, which can restrict material combinations in overmolding applications.
- Surface defects: TPE parts may develop flow marks, weld lines, or uneven surface textures if mold design and processing parameters are not properly controlled.
- Moisture sensitivity during processing: Some TPE grades absorb moisture, which can cause bubbles, surface imperfections, or other molding defects if the pellets are not properly dried.
What is TPE Injection Molding
TPE injection molding, also known as thermoplastic elastomer injection molding or TPE molding, is an injection molding technique where TPE materials are melted and injected into a mold cavity to form specific shapes. This process is widely used in industries requiring flexibility and durability, such as automotive (e.g., seals, gaskets), consumer goods (e.g., soft-touch grips), and medical devices (e.g., tubing, seals) due to their versatility and recyclability.
TPE Injection Molding Process
The TPE injection molding process involves several stages, from preparing the raw material to ejecting the finished part. Each stage affects material flow, dimensional accuracy, and final part quality.
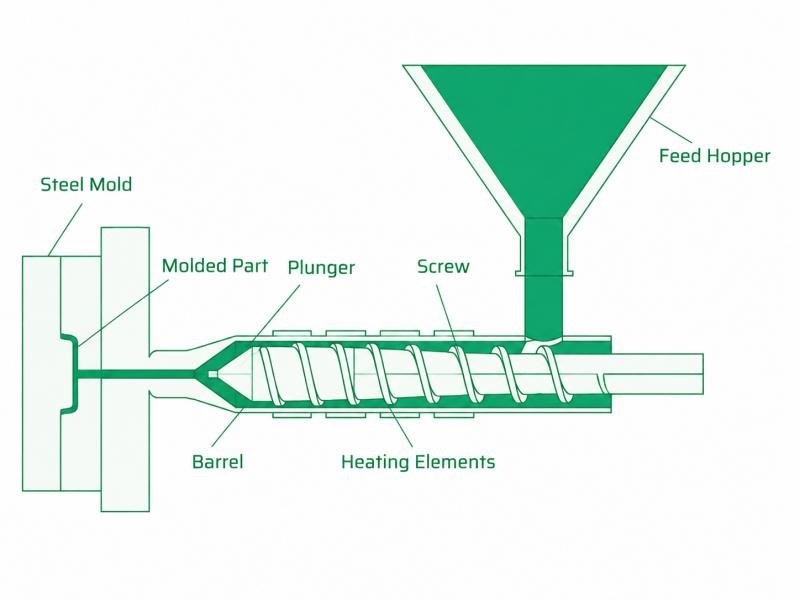
Step 1: Feed and Prepare TPE Pellets
TPE pellets are fed into the injection molding machine through a hopper. The screw conveys the pellets forward, heating and melting them through external heat and mechanical shear.
Step 2: Inject Molten TPE into the Mold
The machine injects the molten TPE into the closed mold under controlled pressure and speed. The material flows through the runner and gate system to fill the cavity and form the required part geometry.
Step 3: Pack and Cool the Material
Holding pressure helps compensate for material shrinkage as the TPE cools. The mold temperature and cooling time must be controlled to maintain dimensional stability and prevent deformation.
Step 4: Open the Mold and Eject the Part
Once the part has sufficient rigidity, the mold opens and the ejection system releases it from the cavity. Because TPE is flexible, appropriate draft angles and ejection settings help prevent stretching or tearing.
Step 5: Inspect and Finish the Part
The molded part is checked for dimensions, surface defects, and other specified quality requirements. Additional operations, such as trimming excess material, assembly, or surface finishing, may follow when required.
TPE injection molding supports repeatable production with relatively short cycle times. Proper control of each stage helps maintain consistent part quality across production runs.
Types of Thermoplastic Elastomers
TPEs are a class of polymers and are categorized into several types based on their chemical structure and properties, each offering unique advantages for specific applications. Below is a detailed breakdown:
Common TPE Injection Molding Issues
TPE injection molding can produce some defects that affect part appearance, dimensions, and functional performance. Identifying the causes helps improve molding consistency and reduce material waste.
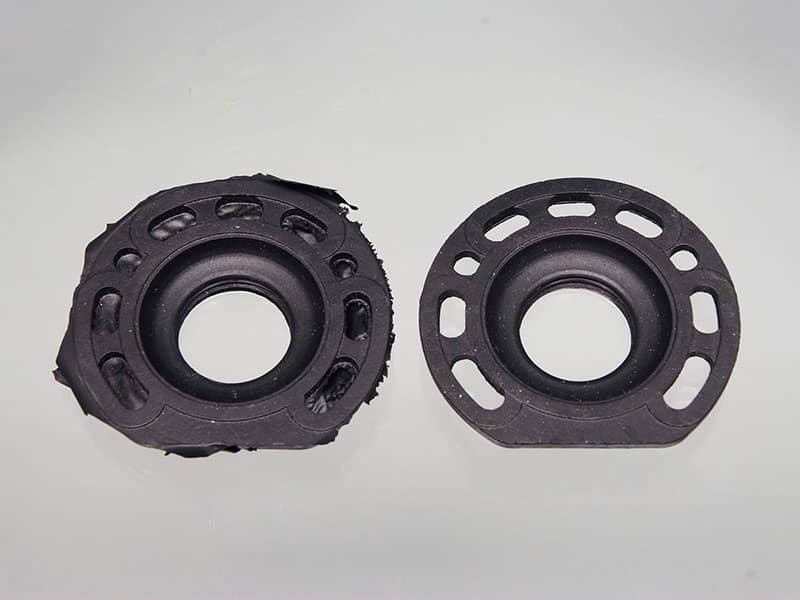
Flash
Flash occurs when molten TPE escapes through the parting line or gaps between mold components. Excessive injection pressure, insufficient clamping force, or worn mold surfaces can cause this defect. Injection pressure and clamping force should be properly adjusted, while regular mold maintenance and gap inspections help prevent flash.
Short Shots
Short shots occur when molten TPE fails to fill the entire mold cavity. Low melt temperature, insufficient injection pressure, or restricted flow through narrow gates can contribute to incomplete filling. Optimizing the melt temperature, increasing injection speed, and checking the gate dimensions can ensure sufficient material flow.

Sink Marks and Warpage
Sink marks appear as depressions on the part surface, while warpage causes the part to deviate from its intended shape. Uneven wall thickness, insufficient holding pressure, and inconsistent cooling can contribute to these defects. Wall thickness should remain consistent throughout the part, with appropriate packing pressure and cooling time to minimize shrinkage and warpage.

Burn Marks
Burn marks appear as dark or discolored areas on molded TPE parts. Excessive shear heating, material degradation, or inadequate mold venting can cause discoloration. Adjust injection speed and melt temperature, and improve venting where necessary.

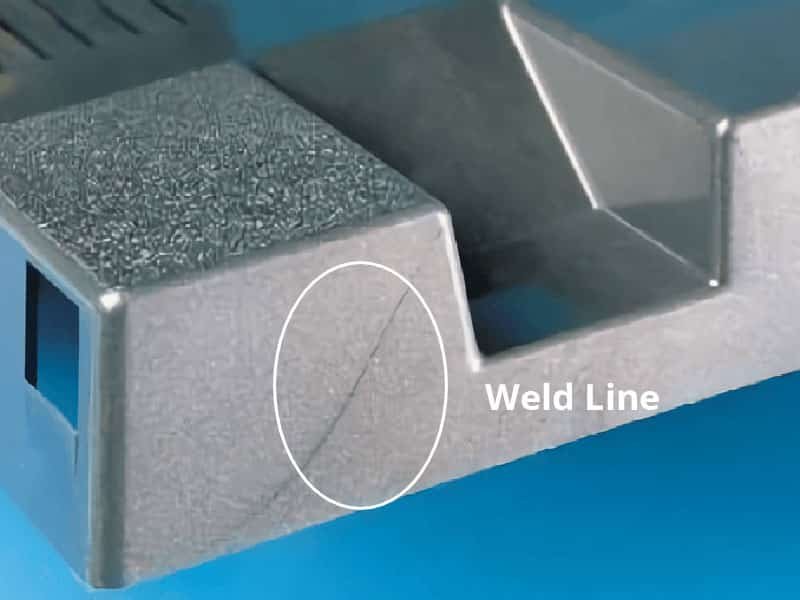
Weld Lines
TPE parts may develop flow lines, weld lines, or uneven textures that affect their appearance. Inadequate melt temperature, inconsistent filling, and unsuitable gate locations can contribute to these issues. Optimizing material flow and gate location and increasing mold temperature can reduce visible flow marks.
Understanding TPE Injection Molding Lead Times and Production Costs
TPE injection molding lead times and production costs depend on tooling requirements, part complexity, material selection, and order quantity. Understanding these factors helps you plan TPE injection molding projects, manage budgets, and establish realistic delivery schedules.
Production Lead Times
TPE injection molding lead times include mold fabrication, initial sampling, design adjustments, and production. Parts with complex geometries or strict dimensional requirements may require additional sampling and validation before mass production begins. Material availability and production scheduling also affect the final delivery date.
Tooling Costs and Development Time
In TPE injection molding, mold complexity, cavity count, and required surface finishes affect tooling costs and development time. Simple mold designs generally require less fabrication time, while complex geometries, side actions, and tight tolerances can increase both costs and lead times.
Material and Production Costs
TPE injection molding material costs vary by grade, hardness, formulation, and performance requirements. Production costs also depend on part weight, molding cycle time, machine requirements, and order quantity. Larger production runs can spread tooling costs across more parts, reducing the tooling cost per unit.
Erye has years of experience in injection molding. We have compiled 12 Useful Tips to Reduce Injection Molding Cost for you.
Applications of TPE Injection Molding
TPE injection molding produces flexible, resilient parts that combine rubber-like behavior with the processing advantages of thermoplastics. Its applications span industries that require cushioning, sealing, grip, or flexible connections.
Automotive Components
In the automotive industry, TPE is used for seals, gaskets, protective covers, soft-touch interior trim, and flexible grips. Its elasticity helps create tight-fitting components, while suitable grades can withstand exposure to weather and automotive fluids.

Medical and Healthcare Products
Selected TPE grades are used for tubing, seals, flexible connectors, and grips on medical devices. Material selection should account for biocompatibility, sterilization methods, and applicable regulatory requirements.

Consumer Products
TPE is commonly used in consumer electronics production for toothbrush grips, tool handles, wearable product components, and protective cases. Its soft-touch feel, flexible design options, and range of hardness levels support ergonomic and comfortable product designs.

Electrical and Electronic Products
TPE is used for cable jackets, flexible protective covers, seals, and strain-relief components. Its flexibility helps protect connections from bending stress, while electrically insulating grades suit applications that require insulation.

Industrial Equipment
Industrial applications include vibration-damping pads, protective boots, flexible seals, and anti-slip handles. TPE can absorb impact and provide cushioning, helping protect equipment and improve handling.

Household Products
TPE is used in non-slip feet, flexible lids, grips, and soft sealing components. Its moldability allows manufacturers to produce parts with varied shapes, textures, and hardness levels for everyday use.

Other Manufacturing Process: Overmolding with TPEs
Overmolding enhances part functionality, such as adding grips to tools or seals to electronics, expanding TPE’s application scope. The process involves molding TPE over a substrate to create parts with combined properties, such as soft-touch surfaces or enhanced grip. It’s a significant application for TPEs, particularly in consumer and medical products.
Material Selection for TPE Overmolding
- Substrate Material: Common substrates include polypropylene (PP), polyethylene (PE), ABS, and polycarbonate (PC). The choice affects adhesion and compatibility.
- TPE Selection: Depends on desired properties like hardness and adhesion. Styrenic TPEs adhere well to polyolefins, while modified TPEs are needed for engineering plastics.
Design Considerations for TPE Overmolding
- Adhesion: Ensure good bonding through chemical or mechanical means, such as textured finishes for mechanical interlocks.
- Wall Thickness: The TPE layer should be thick enough to prevent delamination, with sufficient thickness for functionality.
- Mold Design: Requires multiple cavities or alignment features to accommodate both substrate and TPE, ensuring precise overmolding.
Processing Parameters for TPE Overmolding
- Temperature Control: Manage substrate and TPE temperatures for proper bonding, with high melt temperatures critical for adhesion.
- Injection Speed and Pressure: Controlled to prevent substrate damage, with profiling to ensure uniform flow, as per industry practices.
- Cooling Time: Sufficient to allow bonding, typically longer for overmolded parts, with cooling times of 35-40 seconds per 0.100″ wall thickness for overmolded sections.