What is Insert Molding?
Insert molding is a sophisticated manufacturing process where a pre-formed insert, typically made of metal, plastic, or ceramic, is placed into a mold cavity and then encapsulated with a plastic material, or sometimes an elastomer rubber material. The process combines the insert with the molded material in a single part, allowing the finished component to benefit from the properties of both materials. Insert molding is widely utilized for producing parts that require additional strength, electrical conductivity, or specific properties that plastic alone cannot provide.
Insert Molding Process Overview
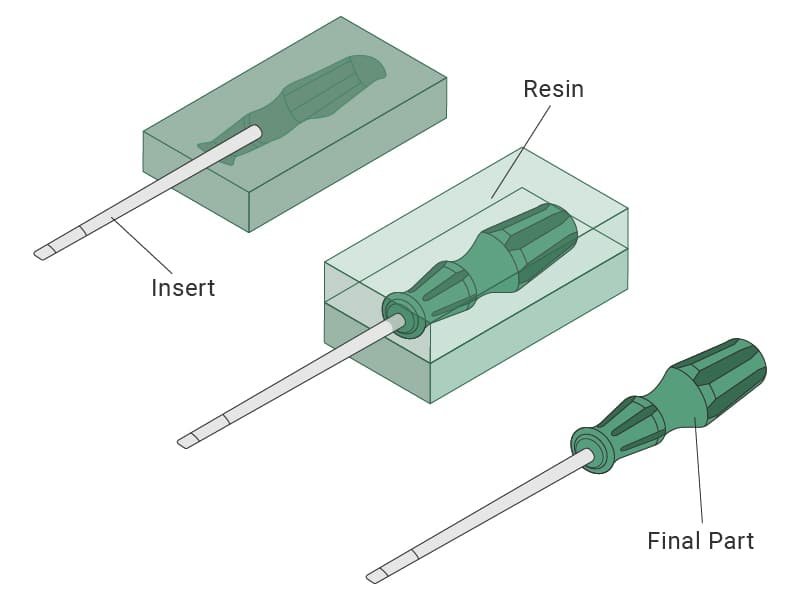
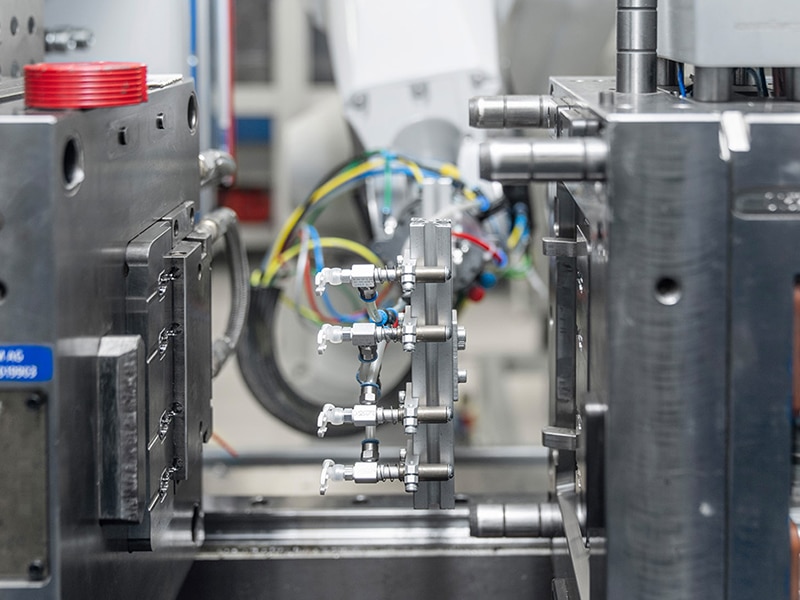
Insert molding begins by selecting and preparing the insert, which can be anything from a metal screw to a ceramic bushing, depending on the requirements of the part. The insert often serves as the load-bearing or functional core of the part. It is placed into the mold cavity, where it is positioned securely to ensure accurate placement during the injection phase.
Next, molten resin is injected under high pressure into the mold, surrounding the insert and forming the final part. The mold is then cooled, and once solidified, the part is ejected. This process provides a seamless bond between the insert and the plastic, offering enhanced durability and functionality. It also reduces the need for secondary assembly and streamlines the production process.
Types of Inserts in Insert Molding
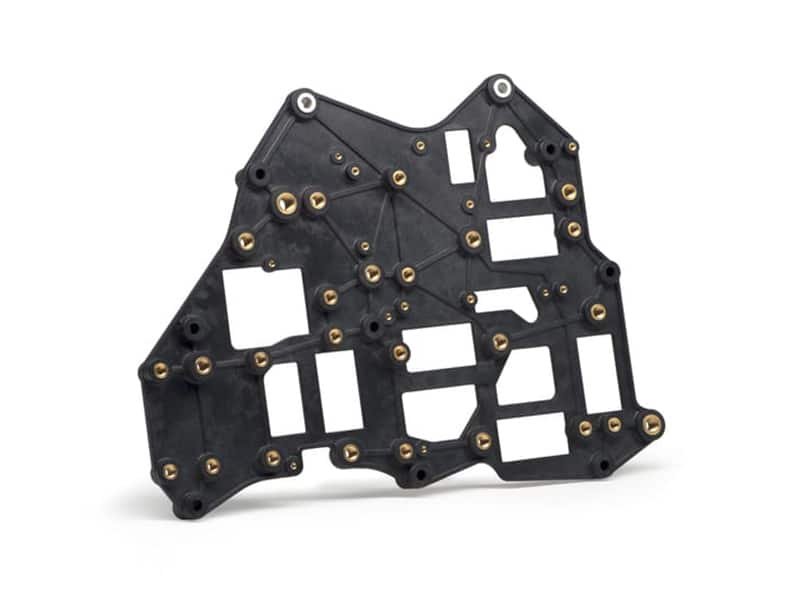
Inserts play a pivotal role in enhancing the performance and functionality of molded parts. By adding inserts with specific properties, insert molding components can meet exacting standards for different industries.
Metal Inserts: Benefits and Applications
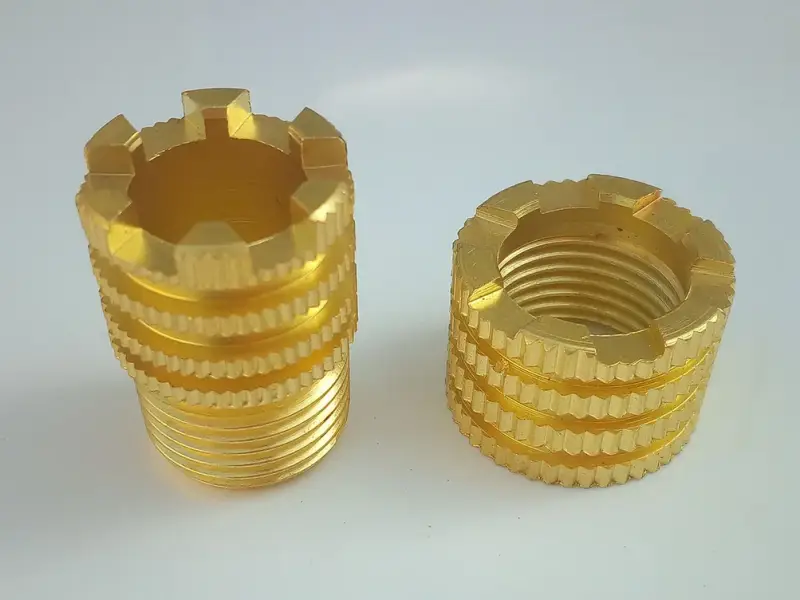
Metal inserts are commonly used in insert moulding for their ability to enhance the mechanical strength and thermal conductivity of the final part. They are ideal for applications that require high strength, such as automotive components, fasteners, and connectors. Metal inserts also provide the necessary hardness and wear resistance for parts subjected to friction or high-impact conditions.
Plastic Inserts: Versatility and Use Cases
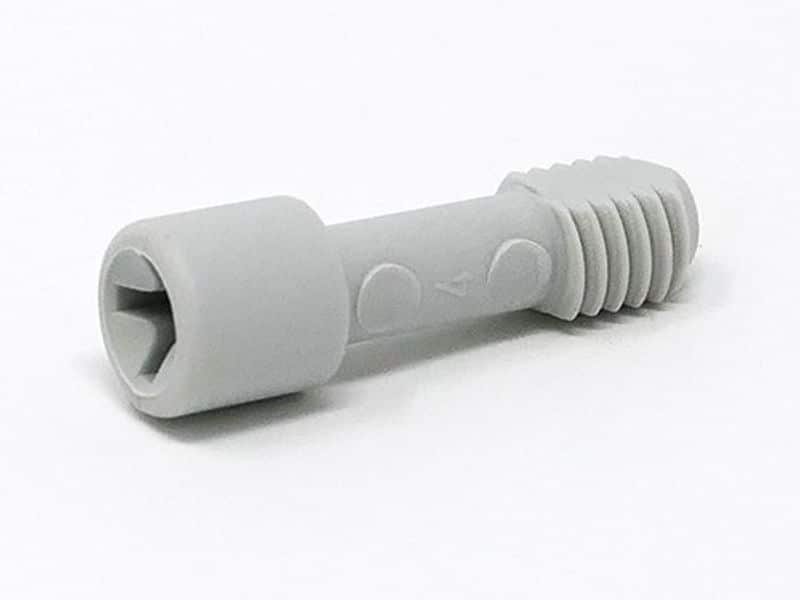
Plastic inserts are often used in insert molding when the primary objective is to enhance the functionality of the part without compromising the overall weight or cost. Plastic inserts are lightweight, versatile, and easy to process, making them suitable for a wide range of applications, from consumer electronics to medical devices. They are often chosen when the part needs to be electrically insulated or requires resistance to chemicals.
Ceramic and Other Specialized Inserts
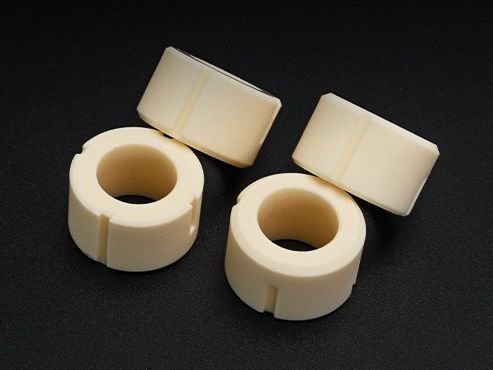
Ceramic inserts are utilized when parts need to withstand high temperatures, extreme wear, or abrasive conditions. These inserts offer excellent thermal resistance and can be used in industries like aerospace and electronics. Other specialized inserts, such as graphite or composite materials, may also be used in insert molding to achieve specific material properties required for the end product.
Common Insert Molding Materials for Molding
The molding material, usually a thermoplastic or thermoset resin, is injected around the insert to create the final part. The material selected must provide adequate bonding with the insert while also meeting the mechanical and functional requirements of the finished product.
Thermoplastics for Insert Molding
Thermoplastics are the most commonly used materials for molding in the insert molding process. These materials are preferred because they can be easily injected into molds, offer good flow characteristics, and can be reprocessed.
- Polycarbonate (PC)
- Acrylonitrile Butadiene Styrene (ABS)
- Polypropylene (PP)
- Nylon (PA)
- Polyethylene (PE)
- Polyetheretherketone (PEEK)
- Polyoxymethylene (POM)
- Polyethylene (PE)
Elastomers and Rubbers for Insert Molding
Insert molding often involves the use of elastomers and rubbers to provide flexibility, cushioning, and high-performance bonding to metal, plastic, or ceramic inserts. Below are some of the most commonly used elastomers and rubbers in insert molding processes.
- Polyurethane(PU)
- TPE
- TPV
- TPU
- Silicone
- Neoprene (Chloroprene Rubber)
- Ethylene Propylene Diene Monomer (EPDM)
- Butyl Rubber (IIR)
- Fluoroelastomers (FKM)
- Nitrile Rubber (NBR)
- Styrene-Butadiene Rubber (SBR)
- Natural Rubber (NR)
Thermosets for Insert Molding
Thermoset plastics are typically used in applications where durability and resistance to high temperatures are required. Once cured, thermosets do not soften or melt, which makes them ideal for high-heat applications or parts that must maintain structural integrity at elevated temperatures.
- Epoxy
- Phenolic
- Melamine
Choose Proper Insert Fit & Lock Features
Ensure the insert has either precise clearance or a press fit based on resin shrinkage. Use knurls, grooves, or undercuts on the insert surface to mechanically lock it in place. But avoid overly aggressive knurls that obstruct flow or cause stress concentrators. For axial loads, embed the insert deep enough—often at least twice the insert’s diameter—to distribute force properly.
Wall Thickness Uniformity Around Inserts
Maintain consistent wall thickness around the insert to avoid uneven cooling, warpage, or sink marks. Where the cross-section changes near the insert, use a gradual transition rather than a sharp change in thickness. Typical wall thickness for many thermoplastics is 1.5-3.5 mm. Thin walls may lead to incomplete fill; thick ones increase cycle time and risk voids.

Suitable Draft Angles & Parting Line Placement
Provide a suitable draft angle (1°-2° or more if surface texture demands) on vertical faces, especially where plastic engages inserts. Avoid locating parting lines through an insert or at a high-stress interface, which can weaken the insert region or cause flash buildup. Proper draft and parting line reduce ejection force and mold damage.
Insert Positioning Relative to Edges & Support Structure
Do not place the insert too close to part edges or thin sections. Maintain at least ~2× wall thickness from insert to nearest edge to prevent cracking during ejection or under load. Ensure there is plastic backing/support beneath the insert so that the load is transferred into the surrounding material, not just the insert.
Threaded Insert Embedding & Orientation
For threaded or functional inserts, ensure the insert is rigidly supported and aligned during molding. Provide sufficient embedment depth and surrounding plastic to keep the insert firmly anchored during use. Also expect sink marks beneath large inserts; avoid showing surfaces under load unless fully supported.
Tooling and Mold Design for Insert Molding
A mold is the foundation of reliable insert molded parts. Mistakes in mold design translate into scrap, defects, or shorter tool life. Here are some useful design considerations.
Choose a Suitable Mold Material and Careful Treatment
Select mold steel grades that match expected wear and temperature cycles. For example, use P20 or 718 steels for moderate runs; hardened steels like H13 or S7 if bulk plastics with fillers or metal inserts are used. Ensure inserts themselves are hardened or plated if they will face abrasion or repeated torque. Heat treatment of mold cavities near the insert seat should minimize distortion over time.
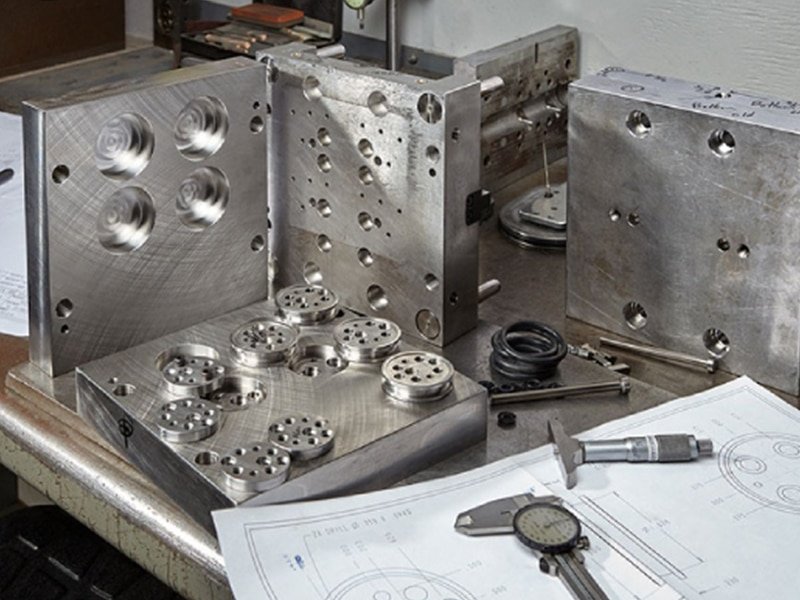
Design Cooling Channels Around Insert Zones
Because metal inserts conduct heat differently from surrounding plastic, mold halves must be designed with cooling channels near insert areas. Maintain a mold temperature differential < 5 °C across the tool near insert pockets to reduce residual stress or warpage. Consider conformal cooling if the cavity geometry is complex.
Gate, Vent, Ejector Layout Near Inserts
Design the gate location so plastic flows toward the insert without creating knit lines that cross the insert faces. Provide vents close to the insert edges to let trapped air escape. Ejector pins should be placed away from inserts or set up so force is evenly distributed—pins should avoid being directly under tight-tolerance insert geometries that would distort or damage them.
Tolerance & Finish for Insert Seating
Tooling surfaces in contact with insert edges or flanges need a tighter finish (e.g., Ra ≤ 1.6 µm or as required) to prevent flash or parting line blemishes. Machined features holding inserts must respect tolerance stack-ups: insert height vs cavity closure, location versus mold shrinkage. Tools should allow periodic maintenance: easy access to replace insert pockets, polish insert seating surfaces, and inspect ejector alignment. For a longer lifetime, coat high-wear regions (e.g., insert pockets) with wear-resistant coatings (nitriding or PVD) if applicable.
Quality Control in Insert Molding
To ensure the highest quality standards, insert molded parts must undergo thorough inspection processes.
Visual inspection is used to identify surface imperfections such as cracks, voids, or flash, which can affect the aesthetic and functional quality of the part.
Dimensional inspection involves measuring key dimensions of the molded part to ensure they align with the specified tolerances. This is often done using precise measuring instruments like calipers, micrometers, or coordinate measuring machines (CMM).
Functional testing evaluates the performance of the part under real-world conditions, ensuring that the insert and molded material bond securely and that the final part meets all mechanical and operational requirements.
Insert Molding vs. Traditional Molding Techniques
Insert Molding vs. Injection Molding
Insert molding shares many similarities with traditional injection molding. Injection molding typically involves only molten plastic being injected into a mold to create a part. Insert molding involves the additional step of placing an insert into the mold before the injection. This allows for the creation of parts that benefit from the strength and functionality of both the insert material and the plastic material.
The main advantage of insert molding is its ability to integrate complex components, such as metal threads or electrical connectors, into a molded plastic part in a single operation. In contrast, injection molding typically requires separate assembly processes for such components.
View our Precision Injection Molding Service
Insert Molding vs. Overmolding
Insert molding and overmolding are both processes that involve adding a secondary material to an existing part, but they differ in their approach and application. In overmolding, a layer of material is applied over a substrate, typically using the same molding material to improve features like grip or protection. In contrast, insert molding involves embedding a separate, pre-formed insert (often made from a different material, such as metal or ceramic) into the molded part.
Overmolding is often used for adding a soft outer layer, like rubber over a plastic base, whereas insert molding is ideal for incorporating functional components, like threaded metal inserts, into a plastic part for strength and durability.
View our Overmolding Service.
Applications of Insert Molding Across Industries
Automotive Industry: Structural Components and Fasteners

In the automotive industry, insert molding is used extensively for creating parts that require both strength and precision, such as structural components and fasteners. Metal inserts, such as steel or aluminum, are often used to reinforce plastic parts that will bear heavy loads or experience stress during operation. Common automotive applications include brackets, connectors, and fasteners that require precise alignment and robust bonding to ensure safety and durability.
Medical Device Manufacturing: Ensuring Precision and Functionality

In medical device manufacturing, insert molding is used to create highly precise and functional parts that meet stringent regulatory standards. For example, metal inserts are often embedded in plastic housings to create secure connections for medical instruments or implants. This allows for the creation of parts with high strength and low weight. The use of insert molding in medical devices ensures that critical parts, like those used in surgical instruments or diagnostics equipment, are reliable, sterile, and long-lasting.
Electronics: Use of Insert Molding for Connectors and Housing
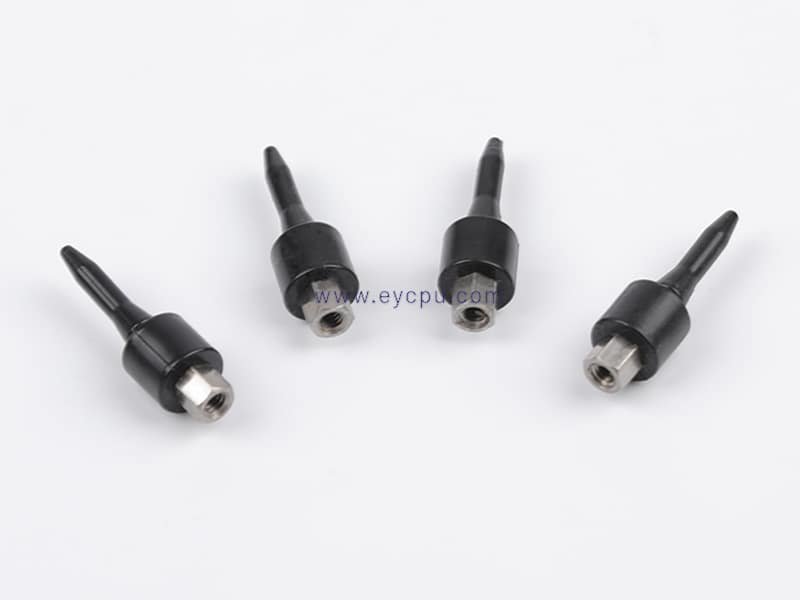
The electronics industry relies heavily on insert molding to create parts that integrate both plastic and metal components. Metal inserts can provide a strong and durable connection point for components like circuit boards, cables, or electrical contacts. The molding process allows for the seamless integration of these components, ensuring a secure fit. Insert molding also enables the creation of complex shapes and intricate designs, making it ideal for the small, precise components often found in electronics.
Consumer Goods: Durability and Aesthetic Applications

Insert molding is also used in the production of durable consumer goods, where aesthetics and functionality must be combined. For example, metal inserts can be used in plastic housings for tools, appliances, or toys, providing structural strength while maintaining a lightweight and visually appealing design. Insert molding can also improve the tactile properties of consumer goods by incorporating soft-touch or ergonomic features, enhancing the user experience.
Industrial Applications: Heavy-Duty Parts and Assemblies

Industrial applications often require parts that can withstand heavy-duty use and extreme conditions. Metal and ceramic inserts are commonly used in industrial applications to provide reinforcement and improve the wear resistance of plastic parts. Insert molding allows for the creation of these high-performance components in a cost-effective manner, with reduced assembly time and fewer potential points of failure.
Choosing the Right Insert Molding Service Provider
Key Criteria for Selecting an Insert Molding Manufacturer
Choosing the right insert molding manufacturer is crucial for ensuring the success of the project. Key factors to consider include the manufacturer’s experience with insert molding, the range of materials they work with, and their ability to meet project timelines. Additionally, it’s important to assess their capacity for high-precision molding, as insert molding often requires exact tolerances and attention to detail. Working with a manufacturer that has a proven track record in the industry ensures that the final product will meet both functional and quality standards.
Assessing Technical Capabilities and Experience
When selecting an insert molding service provider, it’s essential to assess their technical capabilities and experience. A skilled manufacturer will have the knowledge to select the right materials, design the mold, and manage the intricacies of the insert molding process. Experience with various insert types and complex geometries is also important to ensure the manufacturer can meet your project’s specific requirements. Choosing a provider with extensive technical expertise reduces the risk of defects and ensures high-quality production.
Understanding Lead Times, Costs, and Production Schedules
Lead times, costs, and production schedules are key considerations when choosing an insert molding partner. It’s important to align your production timelines with the manufacturer’s capabilities, ensuring they can meet deadlines without compromising quality. Understanding cost structures, including tooling and material costs, is essential for budgeting and assessing the overall value of the project. A reliable service provider should offer transparent pricing and realistic production schedules, helping you plan and manage your project effectively.
How to Collaborate with Your Insert Molding Partner for Best Results
Effective collaboration with your insert custom molding partner is essential for achieving the best results. Clear communication regarding design specifications, material selection, and production expectations ensures that both parties are aligned throughout the project. Regular updates and feedback during the design and prototyping phases help prevent misunderstandings and improve the final product. By working closely with your manufacturer, you can address potential issues early, optimize the process, and ensure that the final product meets all performance and quality requirements.