Scientific injection molding is a structured, data-driven approach designed to achieve consistent part quality and predictable performance. Unlike traditional injection molding methods, it relies on precise control of process parameters and statistical monitoring to minimize variation. This method is increasingly adopted across industries that require high-performance plastic parts, including automotive, medical devices, and consumer electronics.
Principles of Scientific Injection Molding
The core principles of scientific injection molding are the precise control of injection molding parameters. Key variables of the parameters include mold temperature, melt temperature, injection speed, injection pressure, holding pressure, and cycle time. Instead of relying on operator experience and trial-and-error adjustments, this method uses data-driven control to achieve consistent part quality.
For example, mold temperature directly affects material flow and cooling rate, which in turn impacts dimensional accuracy and surface finish. So, temperature must remain consistent to avoid internal stresses and void formation.
Process of Scientific Injection Molding
The injection molding process is typically divided into three main stages:
Fill Phase: Controlled by Injection Speed
During the fill phase, molten plastic is injected into the mold cavity at a controlled speed. The goal is to fill approximately 90-98% of the cavity volume. The speed is optimized rather than using a single constant speed. Different filling speeds may be applied at different stages of cavity filling to ensure smooth material flow and prevent defects.
Injection speed is carefully controlled because it directly affects:
- Melt flow pattern: Injection speed determines how the molten material flows through the cavity, affecting flow balance, filling stability, and material orientation.
- Filling defects: Improper injection speed can lead to defects such as short shots, weld lines, air traps, and burn marks.
- Part appearance: Injection speed has a direct impact on surface quality, including flow marks, gloss variation, and surface defects.
- Dimensional consistency: A stable injection speed helps maintain repeatable filling conditions, improving part-to-part consistency.
Hold Phase: Controlled by Injection Pressure
After the cavity is nearly filled, the process transitions from speed control to pressure control. During this phase, additional pressure is applied to compensate for the natural shrinkage of the plastic material as it cools. Holding pressure and holding time must be carefully optimized. Excessive pressure can create unnecessary stress or make part ejection more difficult, while insufficient pressure may result in shrinkage-related defects.
The hold phase is critical for maintaining:
- Part weight: A consistent hold pressure and hold time help maintain stable part weight from cycle to cycle.
- Dimensional stability: Proper pressure control ensures the molded part maintains the required dimensions after cooling and ejection.
- Internal structure: Adequate holding pressure helps reduce internal voids and improve part integrity.
Cooling Phase: Controlled by Temperature
During the cooling phase, the molded part remains inside the mold until the material reaches a stable temperature and sufficient rigidity for ejection. Scientific injection molding focuses on maintaining consistent mold temperature, cooling time, and heat removal conditions to ensure every part achieves the same performance characteristics.
The cooling phase affects:
- Residual stress and warpage: Uneven cooling can create internal stresses that may cause deformation or dimensional changes after the part is removed from the mold.
- Cycle efficiency: Proper cooling time ensures the part is rigid enough for ejection without unnecessarily increasing the molding cycle.
- Final material properties: The cooling rate influences polymer solidification and crystallinity, resulting in changes to strength, toughness, and dimensional performance.
Key Studies in the Scientific Molding Process
The scientific molding process uses a systematic series of studies. Each study evaluates a specific process variable and uses collected data to determine the optimal settings and establish a robust process window for consistent part quality.
Viscosity Curve Study (Rheology Study)
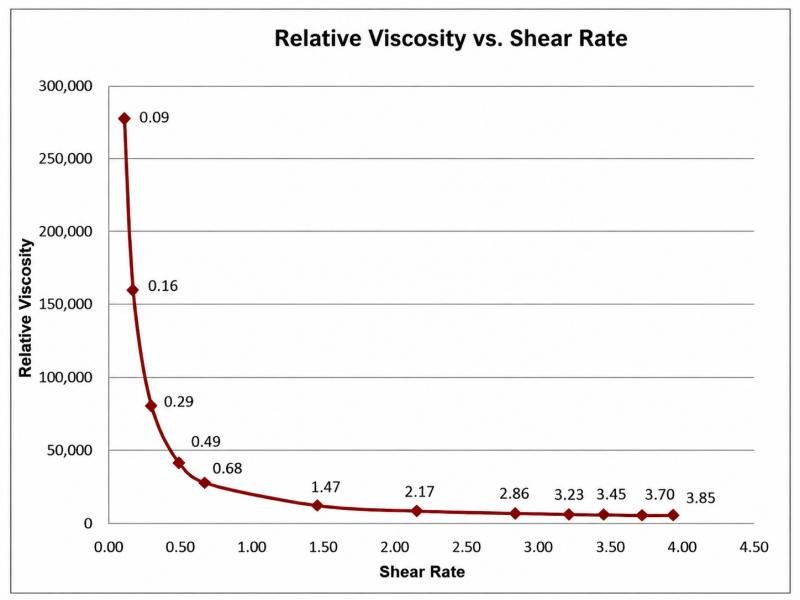
This study identifies the most stable injection velocity for the scientific molding process. Short shots are performed at different injection speeds, while peak pressure and fill time are recorded. Relative viscosity is then calculated as pressure multiplied by fill time, and relative shear rate as the inverse of fill time. A viscosity–shear rate curve is plotted based on these values. A stable filling speed is selected within the plateau region of the curve, where viscosity becomes less sensitive to shear rate, minimizing lot-to-lot material variation.
Cavity Balance Study
This study evaluates fill balance across cavities in multi-cavity molds using short-shot tests ( typically around 95% fill ). Part weights from each cavity are then compared to identify imbalances. Any variation in weight indicates potential issues with runner design, gate sizing, or flow distribution. Then, making adjustments to gate locations, runner diameters, or injection speed until cavity weights are within an acceptable range, typically ±5% or better.
Pressure Drop Study (Pressure Loss Study)
This study measures pressure losses from the nozzle through the runner, gate, and cavity. It conducts incremental shots and records pressures at key points or machine data (using cavity sensors when available). High losses indicate restrictions like small gates, long runners, or sharp geometry changes. The objective is to keep total pressure loss within the machine’s capability to prevent short shots or excessive flash.
Cosmetic Process Window Study
This study defines the range of pack/ hold pressures that produce acceptable surface quality without defects like flash, sinks, or voids. In the study process, pressure is increased in steps until flash appears, then decreased to identify underpacking.
Gate Seal Study (Gate Freeze Study)
This study determines the hold time required to prevent backflow after packing by gradually increasing the hold time in 1-second intervals and measuring part weight at each step. The part weight increases as more material is packed until the gate solidifies and seals the cavity. Once the weight stabilizes, that point is identified as the gate seal time, with an additional 1–2 second safety margin applied.
Process Verification and Documentation
This study focuses on machine-independent parameters, including fill time, transfer position, hold pressure, and hold time. Process templates are developed to enable replication across different machines. During production, cavity pressure sensors and monitoring software such as eDART are used to track process stability. Design of experiments (DOE) is applied to optimize interactions between multiple process variables.
Technology Used in Scientific Injection Molding
Scientific injection molding relies on advanced monitoring and analysis technologies to collect process data and evaluate stability. Key technologies include:
- Cavity pressure sensors: Installed inside the mold to measure pressure changes during filling and packing. The collected data helps evaluate cavity balance, transfer points, holding pressure effectiveness, and part consistency.
- Process monitoring systems: These systems collect real-time data from molding machines and sensors, tracking parameters and helping identify process deviations and maintain stable production conditions.
- Statistical Process Control (SPC) and Cpk analysis: Statistical methods are used to analyze process variation and verify whether the molding process remains capable of consistently producing parts within required specifications.
- Design of Experiments (DOE): DOE is mainly used during process development to study how different variables interact and determine the optimal combination of settings.
Applications and Case Studies
Scientific injection molding is particularly valuable for materials with complex processing behavior, molds with high production demands, and industries with strict quality requirements.
Engineering and Specialty Plastics
Scientific molding is especially beneficial when processing engineering-grade and specialty plastics, such as PEEK, polycarbonate, and nylon. These materials often have narrow processing windows, meaning small changes in temperature, pressure, or cooling conditions can affect part performance. Scientific molding helps keep the molding conditions within the optimal range, ensuring consistent dimensional accuracy.
High-Volume Production with Multi-Cavity Molds
Scientific molding is highly suitable for multi-cavity molds used in large-scale production. Multiple cavities must produce identical parts within the same cycle; even minor process variations can lead to differences between cavities. Scientific molding helps maintain balanced cavity performance and ensures that each part meets the required specifications.
Industry Applications
Industries that require high reliability and repeatable performance often rely on scientific molding to achieve consistent production results and ensure consistent part performance while reducing production variation during large-scale manufacturing. For example, in the medical device industry, the process is used to manufacture precision components that must meet strict quality and regulatory requirements.

Conclusion
Through scientific studies, parameter optimization, and continuous monitoring, scientific injection molding establishes stable processing conditions and maintains consistent part quality. With advanced injection molding capabilities and scientific molding principles, we provide reliable injection molding solutions for complex plastic components across various industries. From material selection and process optimization to precision production, our injection molding services are designed to deliver consistent quality, tight tolerances, and efficient manufacturing results.