
Small batch CNC machining lies between a single prototype and a full production run. It covers batches larger than a one-off prototype, but not enough to justify mass production. For a product team still validating a design or waiting on market demand, this middle ground is where small batch CNC machining fits best. This guide breaks down what small batch CNC machining actually involves, how it differs from prototyping, which processes and materials work best, what drives cost, and how to design parts correctly.
What Is Small Batch CNC Machining
Small batch CNC machining is one of several CNC machining processes used across manufacturing, producing precision parts in quantities typically ranging from 10 to 1,000 units. Compared with large-volume manufacturing, the process can support applications where only a defined number of parts is required, such as functional testing, assembly verification, product evaluation, and replacement components. Because production can be adjusted according to the immediate requirement, it provides greater flexibility when part quantities, specifications, or design details may change during production.
Small Batch CNC Machining vs. Prototyping
Although both may involve relatively small quantities, prototyping and small batch production serve different purposes and follow different production requirements.
Prototyping
Prototyping is aimed at solving design problems. It checks fit, tests an assembly, demonstrates the required concept, or catches a design flaw early. Finish quality and dimensional consistency across pieces matter less, since these parts exist to inform the design, not to be sold or put into service. A prototype order usually gets one setup and a quick finish pass, and it is usually not produced again because the design may change before it is reused.
Small Batch Production
Small batch machining is intended for parts that have reached a stable design and require consistent production in limited quantities. Each batch must reproduce the same dimensions, appearance, and functional characteristics. Achieving this consistency requires a controlled machining process, including defined fixturing, tool paths, machining parameters, and inspection criteria. If the design is still changing between orders, the work is still prototyping, even at fifty units. Once the design is frozen and orders are placed repeatedly against it, the work has moved into small batch production.
Common Processes Used in Small Batch CNC Machining
The processes behind a small batch are the same as CNC machining methods used at any volume. You can choose to use these methods based on the specific geometric shape of the parts.
CNC Milling/ CNC Turning
CNC milling can shape flat faces, pockets, slots, and contoured surfaces in a single setup on one machine, without switching between separate stations. For cylindrical or rotationally symmetric parts, CNC turning offers the same setup efficiency on a lathe instead. They can avoid extra setups and keep machining time down on a small batch.
Swiss-Style Turning
Material stays supported close to the cutting point, which reduces deflection and holds tighter tolerances on slender parts. That precision leads to a slower cutting pace, which makes it impractical for large production volumes but well suited to a small batch.
Wire EDM
Erodes sharp internal corners or hardened materials using an electrically charged wire, without heat distortion. This approach is too slow and costly to apply across a large production volume, but workable for the handful of parts in a small batch that need it.
Multi-Axis Machining
Multi-axis machining rotates the tool or part during the cut to reach compound angles without building a separate custom fixture for each face. Skipping that fixture work matters more on a small batch, where the cost of custom tooling would otherwise fall on very few parts.
Materials Used for Small Batch CNC Machined Parts
Material in small batch machining will influence the part’s appearance and how well parts hold up over time. Choosing materials correctly keeps a batch durable, precise, and visually consistent.
- Aluminum: It is fast to machine and holds tight tolerances well, making it a cost-effective choice when a small batch needs to move through machining quickly.
- Brass: It machines easily and produces a clean surface, reducing the need for additional finishing on a small number of parts, which is cost-effective for small batch machining.
- Stainless Steel, Titanium & Engineering Plastics: These materials offer strength, heat resistance, corrosion resistance, or low friction but involve higher machining or material costs, which have less impact when only a small number of parts require these properties.
Key Advantages of Small Batch CNC Machining
Because small batch CNC machining involves fewer parts and shorter production cycles, it offers some advantages in how materials, time, design updates, and quality consistency are managed.
Less Material Waste
Small batch orders leave less unused material as inventory once the order is complete, since the total volume purchased is smaller to begin with. In contrast, large-volume runs often cut extra stock to buffer against defects or future demand. For small batch CNC machining, this lower material commitment helps keep upfront material costs under control.
Faster Turnaround
A smaller quantity takes less total machine time to complete than a large production run of the same part. Fewer parts also mean fewer inspection and finishing steps to work through before the order ships. This usually shortens the time from order to delivery.
Design Flexibility Between Orders
A small batch order commits to only a small number of units at a time, so revising the design before the next order affects few parts. A large-volume order applies one design across thousands of units at once, so the same kind of revision means reworking or scrapping a much bigger quantity.
High Precision and Quality
A small batch order runs through fewer total cutting cycles, so a single tool setup and calibration covers the entire batch without needing mid-run adjustment. A large-volume run cuts through enough material that tool changes or recalibration happen partway through, increasing the possibility of small variations occurring between the parts.
Understanding Small Batch CNC Machining Costs
The pricing for small-batch CNC machining mainly depends on the following factors, and understanding them in advance makes it easier to plan a budget.
- Fixed Cost: Setup costs and material preparation are required for each batch. In a small batch, those costs are divided across fewer parts, raising the price each one carries.
- Material Cost: Higher-cost materials like titanium or certain stainless grades raise the price of a small batch more noticeably than a lower-cost material like aluminum.
- Machining Process Choice: Processes like Swiss-style turning or wire EDM run more expensive than standard milling or turning.
- Design Complexity: Deep pockets, thin walls, or features requiring multiple setups each add machining steps. More steps mean more machining time, which leads to an increase in costs.
- Secondary Operations: Surface finishing like anodizing, bead blasting, tapping, or hand deburring each add a step outside the core machining process, and each added step adds to the final cost.
DFM Best Practices for Small Batch CNC Parts
Small batch orders do not have enough volume to spread the impact of inefficient design choices, which makes DFM considerations especially important before machining begins.
Standardize Hole Sizes
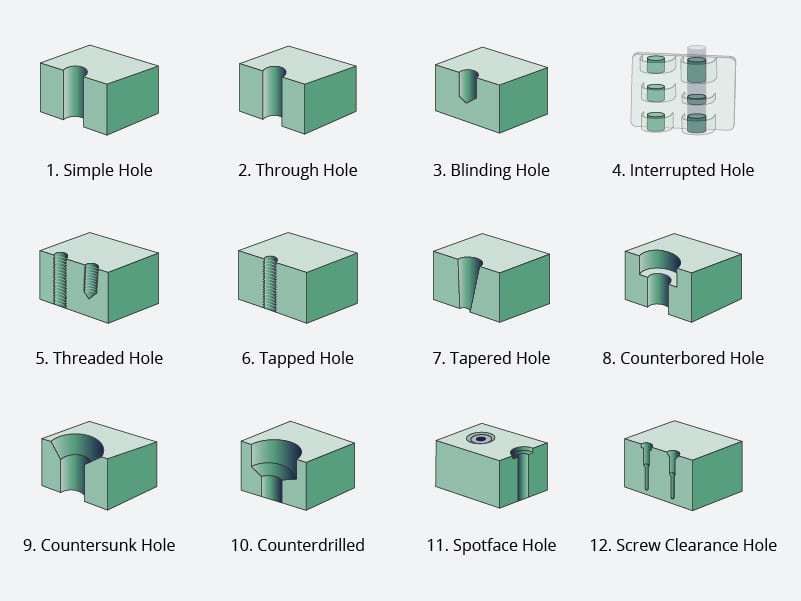
Machined parts need a wide range of hole types. Using fewer hole sizes and keeping similar hole features consistent across the part can simplify the machining process and reduce the number of setups required, keeping machining costs under control.
Avoid Deep and Narrow Pockets
A pocket much deeper than it is wide can only be cut with a long and thin tool, and that tool flexes under cutting pressure. The flex can lead to a decrease in accuracy. Widening the pocket or breaking it into shallower steps avoids such cases, keeping the cut fast and the tolerance tight.
Round Internal Corners
CNC cutting tools are round, which means they naturally leave a radius at internal corners. Adding a matching corner radius allows the part to be machined with standard tools at normal speeds. Sharp internal corners require smaller tools or additional processes such as wire EDM, increasing machining time and cost.
Design Tolerances
A tight tolerance on a mating surface is often necessary. But the same tight tolerance applied uniformly across every dimension on the drawing adds cost with no functional benefit. Only when the part actually needs them should tight tolerances be adopted, and leave the rest at standard machining tolerance.
Getting Started with Small Batch CNC Machining
Small batch CNC machining provides a practical option when production requirements do not justify high-volume manufacturing. Erye’s CNC machining services support small batch projects with precision machining, material guidance, and DFM feedback to help identify potential cost drivers before production and helps maintain consistent quality across the batch.