
Simple Hole
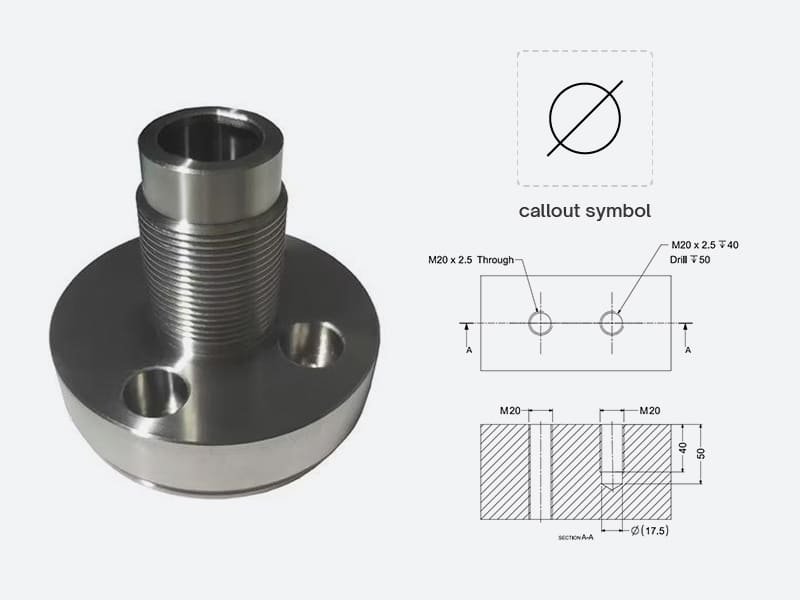
A simple hole is the most basic type of hole used in engineering and manufacturing. It is a cylindrical opening created in a material without any additional modifications such as threading, countersinking, or counterboring. Simple holes can be either through holes or blind holes. In technical drawings, a simple hole is typically represented by a circle with a diameter dimension. It is often denoted as ØD, where “D” represents the hole diameter.

Through Hole
A through hole is a type of hole that passes entirely through a material, creating an opening from one side to the other. This is one of the most common and versatile types of holes used in various engineering applications. Through holes can be designed in a variety of diameters and depths, depending on the material and intended use. In engineering drawings, through holes are represented by a simple circle with the hole’s diameter indicated, and no depth is indicated, as the hole completely passes through the material.
Blind Hole
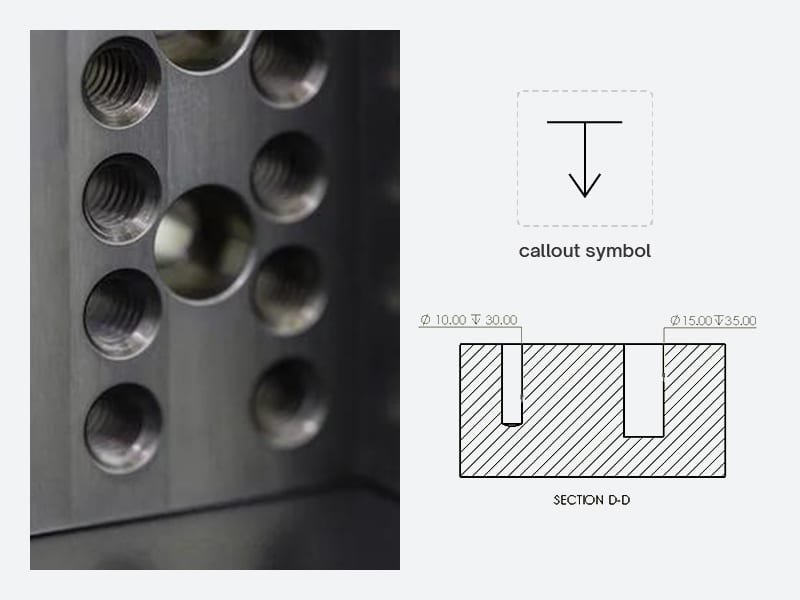
A blind hole is a type of hole that does not completely pass through the material. Instead, it has a bottom, which limits its depth. Blind holes are commonly used in applications where the hole needs to retain a specific depth without penetrating through the entire material, such as for fastening, threading, or for functional purposes in a variety of engineering systems.
In engineering drawings, a blind hole is also marked with its depth, typically represented as H x D, where H is the hole’s depth, and D is the diameter. The notation for a blind hole will often be accompanied by a symbol that indicates that the hole does not pass through the material (such as a “T” or “B” for blind).
Design Tips for Simple Hole
- Hole Diameter Considerations: Ensure proper clearance for fasteners or other inserted components.
- Material Strength: Avoid placing holes too close to the edges of a part to prevent structural weakening. A typical minimum edge distance is 1.5 times the hole’s diameter.
- Tolerance Requirements: Use tighter diameter and positional tolerances for holes that require precise fits or alignment.
- Depth and Diameter Considerations: Blind holes with deep, narrow dimensions can lead to challenges in drilling and the potential for material distortion.
Interrupted Hole
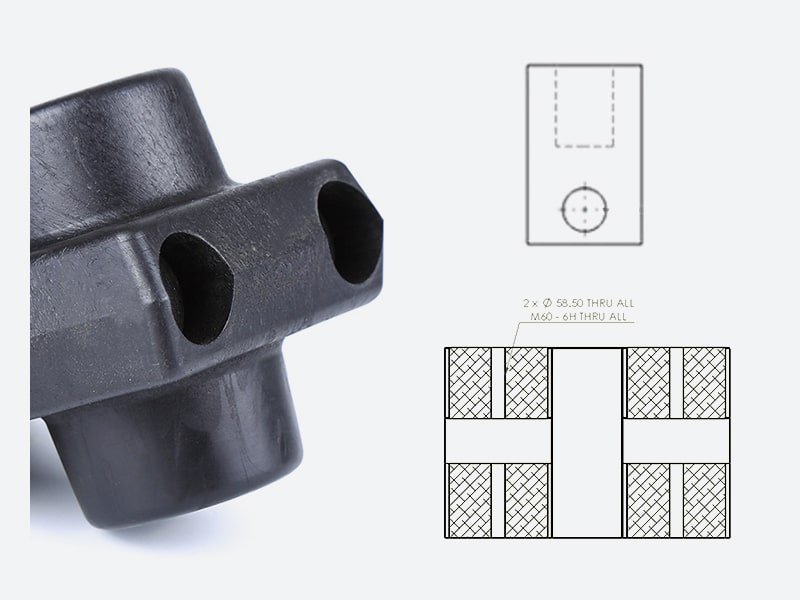
An interrupted hole is a type of hole that features breaks or interruptions along its path, meaning that the hole is not continuous throughout the entire material thickness. These interruptions could be caused by a variety of factors such as non-uniform hole patterns, changes in diameter, or alterations in the geometry of the hole. Interrupted holes are typically designed to accommodate specific functional requirements or manufacturing limitations.
Interrupted Hole Callout Symbol in Engineering Drawings
In engineering drawings, interrupted holes are represented by a typical hole symbol, but with annotations indicating the interruptions. The exact nature of the interruption is typically illustrated through dimensions, and sometimes with additional symbols or dashed lines that mark where the interruption occurs.
Design Tips for Interrupted Hole
- Ensure Uniform Interruptions: Maintain consistent spacing between interruptions (typically 1.5 to 2 times the hole diameter) to avoid stress concentration and ensure part strength.
- Minimize Depth of Interruptions: Keep the interruption depth as shallow as possible while still meeting the functional requirements. Excessive depth can lead to weak points and machining difficulties.
- Use Filleted Edges: Incorporate fillets or radii at the transition points between the interrupted sections. This reduces stress concentrations and minimizes the risk of cracking, especially in materials that are prone to brittle failure.
Thread Hole
A thread hole contains internal threads, allowing it to accommodate a matching external thread, such as a screw, bolt, or threaded rod. Threaded holes provide secure fastening without extra nuts, making them essential in engineering and manufacturing, especially when designing threads for injection-molded plastic parts. They can be formed either by cutting threads into a pre-drilled hole (tapping) or by forming threads through plastic deformation (thread forming).

Tapped Hole
Tapped holes are closely related to threaded holes but refer to the hole prepared for the tapping process. The tapping hole is drilled to the appropriate size before threads are cut, while the threaded hole refers to the finished feature. Simply put, a tapped hole is a type of threaded hole, but not every threaded hole is necessarily tapped. For a clearer explanation of the difference between tapped holes and threaded holes, you can refer to our detailed comparison.

Thread Hole Callout Symbol in Engineering Drawings
Threaded holes are typically represented in engineering drawings using a standard notation that includes:
- The nominal diameter (e.g., M6 for metric threads, ¼”-20 for imperial threads).
- The thread pitch or thread per inch (TPI) (e.g., M6 × 1.0 or ¼”-20 UNC).
- The depth of the thread (if not a through-hole).
- Optional thread class for precision applications (e.g., 2B or 3B for internal threads).
- If a hole requires tapping, it is often labeled with a “TAP DRILL” or “TAPPED HOLE” annotation.
Example: M10 × 1.5 – 20 mm deep (indicating a metric thread with a 10 mm diameter, 1.5 mm pitch, and 20 mm depth).
Design Tips for Thread Hole
- Choose the Right Thread Type: Use metric threads (ISO) for global applications or UNC/UNF for U.S. standards.
- Proper Drill Size: Always use the correct pre-drill size to maintain thread strength; for instance, an M10 × 1.5 thread requires an 8.5 mm pilot hole.
- Thread Engagement: Aim for a thread depth of at least 1.5× the bolt diameter in steel and 2× in softer materials like aluminum for optimal strength.
- Avoid Over-Tightening: Excessive torque can strip internal threads, particularly in softer materials. Consider using thread inserts (e.g., Helicoil) for reinforcement.
- Chamfer the Entry: Adding a small chamfer at the hole opening allows for easier thread cutting and improves alignment when assembling parts.
Tapered Hole
A tapered hole is a hole that gradually narrows from the entrance to the bottom, creating a cone-like shape. These holes are commonly used when there is a need for a snug fit or for applications where the part needs to hold a tapered pin or a fastener. Tapered holes are often designed for applications where assembly or alignment requires a gradual fit, such as in certain types of mechanical and hydraulic systems.
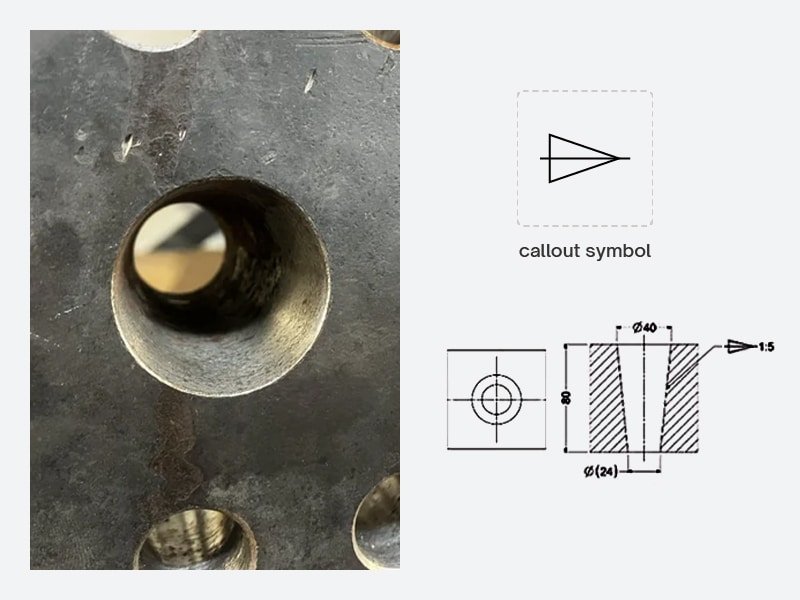
Callout Symbol in Engineering Drawings
Tapered holes are specified with a combination of diameter, taper ratio, and depth. The notation typically includes the large diameter (D), the taper per unit length (e.g., 1:20), and the depth of the hole. For example:
Ø10 × 1:10 × 30mm deep → This represents a tapered hole with a 10mm opening diameter, a taper ratio of 1:10, and a depth of 30mm.
For pipe threads, standard designations such as NPT (National Pipe Tapered), BSPT (British Standard Pipe Tapered), and ISO Metric Tapered Threads are commonly used in callouts.
Design Tips for Tapered Hole
- Angle Consideration: The taper angle is critical to ensure the proper fit of the component. A typical taper angle can range from 1 to 5 degrees, but the angle depends on the application and material.
- Fit Tolerance: Ensure that the tolerance of the hole matches the specific requirements of the part that will be inserted into it. The fit should not be too tight or too loose to avoid assembly issues.
- Chamfering: Adding a chamfer at the entrance of the tapered hole can ease the assembly process and help guide the tapered pin or bolt into the hole.
Counterbore Holes
A counterbore hole is a cylindrical hole that has a larger diameter at the top, allowing for a flat-bottomed recess. This type of hole is commonly used to accommodate the head of a bolt, screw, or other fasteners that require a flush or recessed fit with the surface of the part. Counterbore holes are typically used when the fastener needs to sit below the surface to prevent protrusion or to allow for a smooth, even surface finish.
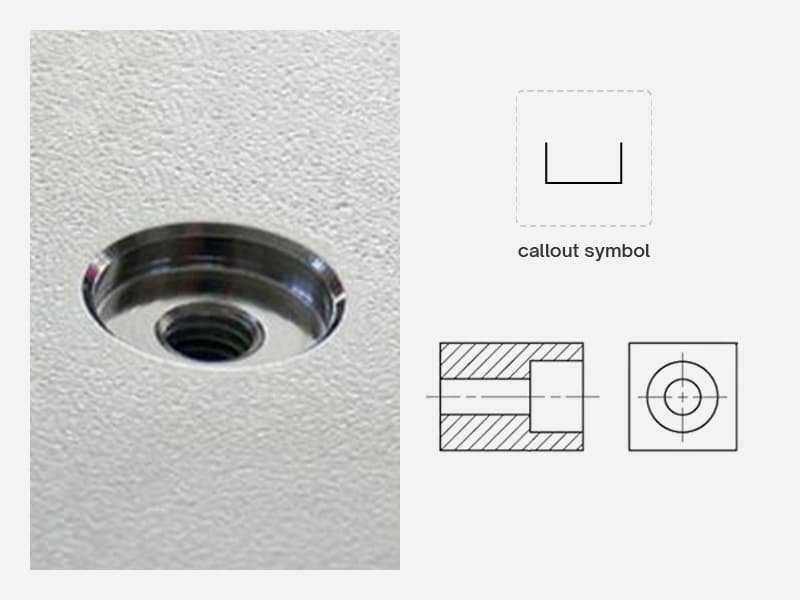
Counterbore Hole Callout Symbol in Engineering Drawings
In engineering drawings, a counterbore is represented by two diameters: the larger diameter for the counterbored section and the smaller diameter for the main hole. The callout is typically represented as ØD1 × D2, where D1 refers to the diameter of the main hole, and D2 refers to the diameter of the counterbored section. The depth of the counterbore is also indicated.
For example, a counterbore hole with a main hole diameter of 10mm and a counterbore diameter of 20mm at a depth of 5mm would be represented as Ø10 × 20 (5).
Design Tips for Counterbore Hole
- Correct Fastener Size: Ensure that the counterbore’s diameter is designed to match the size of the fastener head.
- Depth Control: The depth of the counterbore must be sufficient to house the fastener head completely, ensuring it doesn’t protrude or leave a gap.
Countersink Hole
A countersink hole is a type of hole with a conical recess at the opening, which enlarges at the top to allow a fastener, typically a screw or bolt, to sit flush with or slightly below the surface of the material. This design is commonly used with flat-head screws to prevent the screw head from protruding and maintain a smooth exterior surface.
Both countersink and counterbore holes provide a recessed area at the hole opening to accommodate a fastener head, but their recesses have different shapes and serve different fastener designs. For a detailed comparison of these two hole features, you can refer to our guide on countersink holes vs counterbore holes.
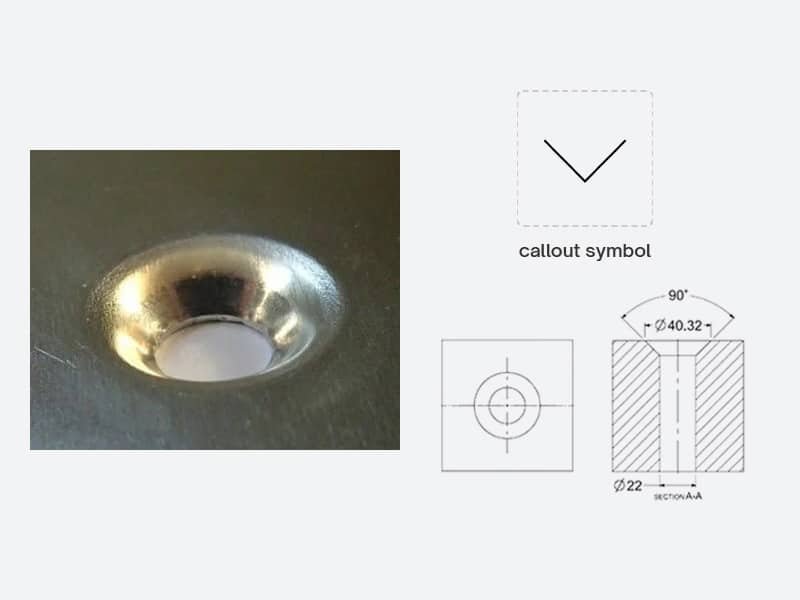
Callout Symbol in Engineering Drawings
In engineering drawings, a countersink hole is represented by a single diameter for the hole and an angle for the countersink. The angle is typically 82°, the standard for most screws, but can vary based on the screw type. The callout is typically shown as ØD × A, where D is the diameter of the hole, and A is the angle of the countersink.
For example, a countersink hole with a diameter of 8mm and a 90-degree countersink angle would be represented as Ø8 × 90.
Design Tips for Countersink Hole
- Correct Angle and Size: Ensure the countersink angle corresponds to the required fastener angle (typically 82°, 90°, or 100°) to ensure proper seating of the screw head.
- Ensure Adequate Depth: The countersink depth must be sufficient to accommodate the fastener head fully, ensuring it sits flush with the surface without being too shallow or deep.
- Avoid Stress Risers: Don’t create deep countersinks in high-stress areas to prevent cracks.
Counterdrill Hole
A counterdrill hole is a type of hole that is drilled to a specified depth to create a stepped or recessed profile within the hole. It is often used when a part requires multiple depths within the same hole, providing a precise fit for different types of fasteners or components.
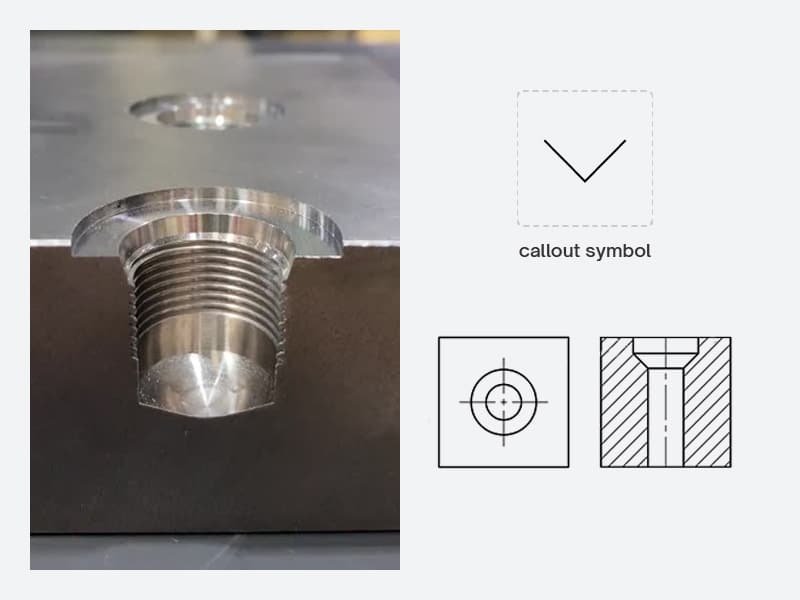
Counterdrill Hole Callout Symbol in Engineering Drawings
In engineering drawings, the counterdrill hole is typically represented by two diameters: the top diameter and the bottom diameter, along with the depth of the hole. The symbol for a counterdrill hole can be denoted as ØD1 × ØD2 × H, where:
- D1 is the diameter of the top of the hole.
- D2 is the diameter at the bottom of the hole.
- H is the depth of the hole.
For example, a counterdrill hole with a top diameter of 10mm, a bottom diameter of 6mm, and a depth of 8mm would be represented as Ø10 × Ø6 × 8.
Design Tips for Counterdrill Hole
- Hole Diameter Tolerances: Maintain precise diameter tolerances, typically ±0.1mm, to ensure proper fitment with fasteners and prevent misalignment.
- Hole Depth vs. Diameter Ratio: Keep the depth-to-diameter ratio below 4:1 to avoid tool deflection and ensure accurate hole geometry.
- Edge Distances: Ensure a minimum edge distance of 2-3 times the hole diameter to prevent material failure or cracking around the hole.
- Chamfer and Deburring: Apply a 45° chamfer to the hole edge to eliminate sharp corners and ease the insertion of screws or fasteners.
Spotface Hole
A spotface hole is a flat or slightly recessed surface machined around a hole, typically used to provide a smooth and even bearing surface for a bolt or other fastener. Spotfacing is often done when the surrounding area of a hole is rough or irregular, and it’s crucial to ensure proper seating for fasteners, ensuring stability and preventing damage to the surrounding material.

Spotface Hole Callout Symbol in Engineering Drawings
In engineering drawings, a spotface hole is represented by a circle symbol with a notation indicating the diameter of the spotface and its depth. The callout might look something like ØD × H, where:
- D is the diameter of the spotface.
- H is the depth of the spotface recess.
For example, a spotface with a diameter of 10mm and a depth of 2mm would be notated as Ø10 × 2.
Design Tips for Spotface Hole
- Spotface Diameter: The spotface diameter should be slightly larger than the bolt or fastener head, typically by about 1.5-2 times the diameter of the fastener.
- Spotface Depth: Depth should be kept between 0.5 and 1.5 times the diameter of the fastener to ensure proper seating without excessive material removal.
- Surface Finish: Ensure a smooth finish, aiming for a Ra of 1.6 to 3.2 microns for a secure fastener fit and to reduce the chances of wear or loosening.
- Edge Distance: Maintain at least 2 times the diameter of the fastener between the spotface and the edge of the material to avoid material deformation and ensure strength.
Screw Clearance Hole
A screw clearance hole is a type of hole designed to allow a screw or bolt to pass through without engaging with the threads of the fastener. These holes are essential in ensuring that the screw or bolt can move freely through the material, providing a secure fit when the fastener is tightened.
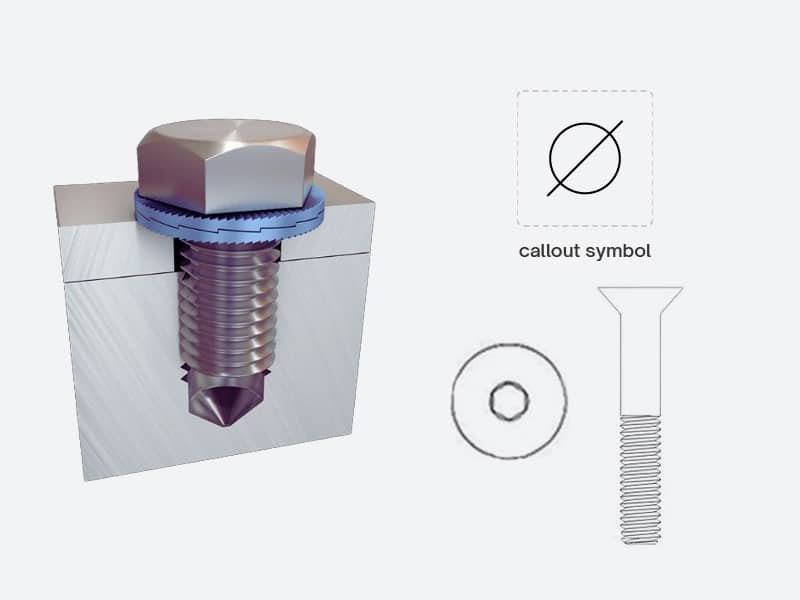
Callout Symbol in Engineering Drawings
In engineering drawings, a screw clearance hole is typically represented as a simple circle with a diameter specified larger than the screw’s nominal diameter. The callout will indicate the diameter of the clearance hole, often denoted as ØD, where D represents the diameter of the hole.
For example, for a screw with a nominal diameter of M6 (6mm), the screw clearance hole might have a diameter of Ø8, ensuring that the screw can pass through without interference.
Design Tips for Screw Clearance Hole
- Hole Diameter Selection: The screw clearance hole should be 0.2mm to 0.5mm larger than the screw diameter to allow smooth insertion.
- Hole Depth: The hole depth should typically be 1.5 to 2 times the length of the screw for proper fit.
- Material Considerations: Softer materials may require a slightly larger clearance hole to prevent deformation.
- Tolerance and Fit: Use standard tolerances like ISO 2768 or tighter fits such as H7 for precision applications.
Common Methods for Machining Holes
There are several methods for machining the different types of holes in engineering. The following are some of the most commonly used methods.
Drilling
Drilling is the most straightforward and commonly used method for creating holes. A rotating drill cuts directly into the workpiece to produce the initial hole, making it suitable for standard holes such as through holes, blind holes, and screw clearance holes. Hole diameter and depth are primarily controlled by the selected drill and programmed machining parameters.
Boring
If you need to achieve higher accuracy, particularly for large diameter holes, boring is often the next step. Boring enlarges an existing hole to achieve tighter tolerances and better surface finish. It is commonly used after drilling to refine the hole dimensions.
Reaming
Reaming is used to refine the hole after drilling. This process removes a small amount of material to achieve a more precise and smoother finish. It’s often applied to holes that need to meet tight tolerances or to create holes with a very smooth interior surface, which is critical for applications like press-fit assemblies.
Tapping
Tapping is used when you need to create internal threads in a hole. A tap tool is inserted into the hole and rotates to form threads on the inside surface. This is crucial when screws or bolts need to be inserted securely into the material. Tapping is typically used after drilling the hole to the appropriate diameter for the threads required.
Milling
The CNC milling process can be employed for both hole creation and surface preparation. A rotating cutter removes material to create complex hole shapes, such as square or irregular profiles, which cannot be easily achieved with simple drilling. Milling is commonly used for features like counterbores and countersinks.
The table below helps you quickly identify the machining processes commonly used for different types of holes.
| Machining Process | Applicable Hole Types |
|---|---|
| Drilling | Simple Hole, Through Hole, Blind Hole, Screw Clearance Hole |
| Boring | Blind Hole, Through Hole, Tapered Hole |
| Reaming | Blind Hole, Through Hole, Tapered Hole |
| Tapping | Tapped Hole, Threaded Hole |
| Milling | Counterbore Hole, Countersink Hole, Counterdrill Hole, Spotface Hole, Interrupted Hole |
How to Choose a Hole Type
Choosing the right hole type depends on the hole’s function, how the part will be assembled, and the required precision, cost, and maintenance.
Consider the Hole Function
A through hole is suitable when the hole needs to pass completely through the part, while a blind hole is used when the hole must stop at a specific depth. A tapered hole suits tapered mating components, while an interrupted hole is appropriate when another feature crosses or interrupts the hole.
Consider Assembly Needs
The fastener or mating component often determines the hole type. A screw clearance hole allows a fastener to pass through. A counterbore hole or countersink hole can accommodate the fastener head, while a spotface hole provides a flat seating surface. A counterdrill hole is suitable when different diameters are needed within the same hole.
Balance Cost and Requirements
Hole complexity can affect machining time and overall part cost. Simple holes are generally more economical when they meet the functional requirements, while counterbores, countersinks, counterdrills, and other specialized features require additional features and may increase production costs. Choose a specialized hole type when its functional or assembly benefit justifies the additional cost.
Space and Part Geometry
Available space and surrounding features can affect the choice of hole type. A blind hole may be preferable when a through hole would interfere with other features, while counterbores, countersinks, and spotfaces require sufficient space around the hole. Reviewing these factors through DFM design can help identify potential issues before machining.
Conclusion
Different hole types serve different design purposes. A hole should not be selected simply by its shape. Its geometry needs to work with the part, the mating components, and the purpose of the assembly. In practice, the best choice is usually the hole type that meets the functional requirement without adding unnecessary complexity.
For parts with multiple or precision hole features, our CNC machining service supports the required machining and inspection processes to produce holes according to the specified design requirements.